HROUS
Rockwell Hardness Testing: Australian Buyers’ Lab Requirements
For a Rockwell hardness lab order, identify the component and governing specification, match the required method, scale and specimen category to the laboratory’s NATA scope, then agree on preparation, test locations and reporting. The scopes distinguish methods and specimen categories; general accreditation alone does not establish the match. [2][3][4]
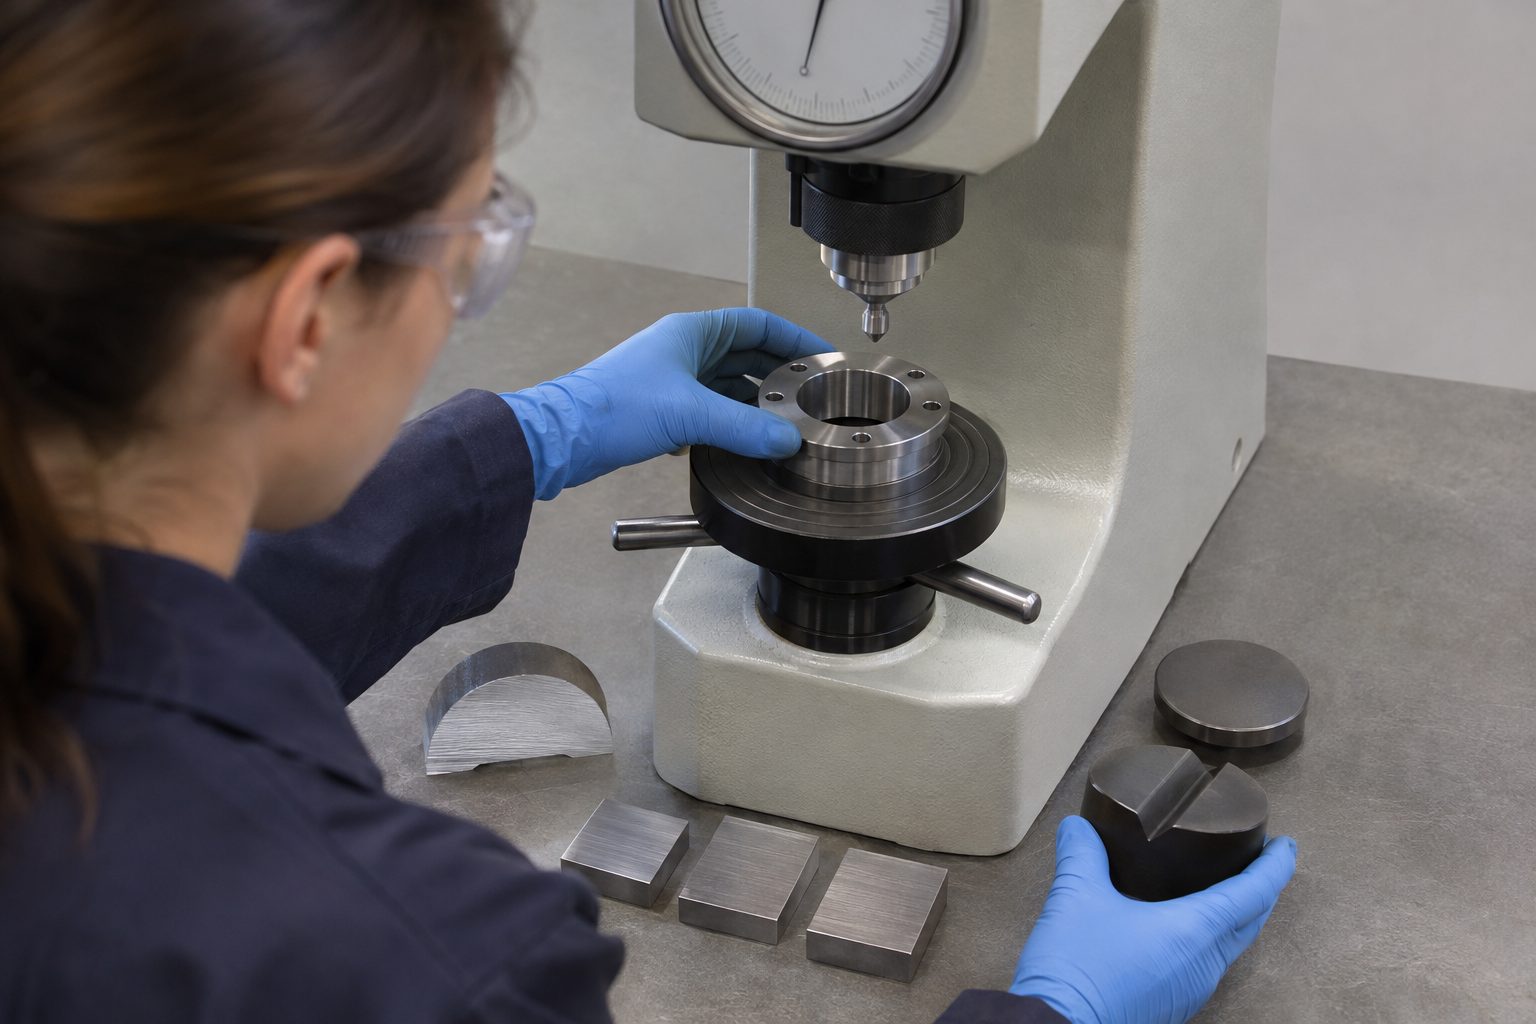
Separate specification requirements from recommended ordering controls:
- Required by your specification: reproduce its method, scale, acceptance limits and any preparation or location requirements.
- Scope check: identify the component-testing entry covering the proposed specimen category, method and scale. [2][3][4]
- Recommended customer instructions: provide sample identifiers, preparation permissions, marked locations and report references. The cited pages for Perth NDT, Victorian Testing, AMTS and LMATS do not state a complete mandatory submission checklist. [2][3][4][5]
1. Identify the component and acceptance requirement
Give each component a unique sample identifier and use it consistently in the order and supporting documents. As recommended order information, include:
- Component identity: description, quantity and sample identifier for each item.
- Document references: part number, drawing number and revision, and purchase-order reference.
- Material identity: material or grade, plus the heat or batch identifier where available.
- Acceptance requirement: attach the governing purchase specification or drawing extract; highlight the test method, edition where specified, Rockwell scale and acceptance limits.
Keep the acceptance criterion separate from the scope entry. The NATA scopes identify testing activities, methods and specimen categories—not your purchase specification’s pass/fail limits. [2][3][4]
If the specification omits the scale, or the drawing and purchase specification conflict, resolve the discrepancy with the person responsible for the requirement before releasing the order. Record the agreed clarification rather than silently selecting a scale or converting an acceptance limit.
2. Match the laboratory’s method, scale and specimen category
The following NATA scope entries show differences across Western Australia, Victoria and Queensland. They are scope comparisons, not a ranking of laboratories. [2][3][4]
Perth NDT and Mechanical Testing Laboratory — Western Australia
- Specimen category: prepared metallic test specimens and welded test specimens. [2]
- Rockwell scales: B and C. [2]
- Methods: AS 1815.1 and ASTM E18. [2]
- Scope boundary: the scope also includes Brinell, portable Brinell and Vickers hardness; ask Perth to confirm any proposed Scale A or portable/on-site Rockwell work separately. [2]
Victorian Testing and Inspection Services – Melbourne Laboratory
- Specimen category: prepared metallic test specimens. [3]
- Rockwell scales: A, B and C. [3]
- Methods: AS 1815.1, ASTM A370 and ASTM E18. [3]
- Scope boundary: its welded-specimen hardness entries cover Brinell and Vickers, rather than Rockwell. [3]
Advanced Materials Testing Services (AMTS) — Queensland
- Specimen category: prepared metallic test specimens, with a separate entry for threaded fasteners, bolts and nuts. [4]
- Rockwell scales: A, B and C for prepared metallic specimens; C for the fastener category. [4]
- Methods: AS 1815.1 and ISO 6508-1 for prepared specimens; AS/NZS 1252.1 clause 6.6.3, AS 4291.1 and AS/NZS 4291.2 for fasteners. [4]
- Scope boundary: match fastener work to its separate entry rather than assuming the prepared-specimen listing covers it. [4]
For prepared-specimen testing to ASTM E18, Perth and Victorian Testing have listed entries; for ISO 6508-1, AMTS has the listed entry. [2][3][4] For a welded-specimen Rockwell requirement, Perth explicitly lists that category. [2]
Treat these as scope matches, not evidence unlisted work is unavailable. Ask the laboratory to confirm the proposed work—including the required hardness range—falls within its accredited entry. Record the relevant laboratory site and scope entry in the purchasing file.
3. Distinguish component testing from machine calibration
A machine-calibration entry is not a component-testing entry, even when both reference the same standards. AMTS’s NATA scope separates prepared-specimen and fastener testing from calibration of Rockwell and superficial Rockwell hardness machines. [4]
The calibration service compares machines with a reference standard and includes on-site calibration. Its superficial Rockwell machine-calibration entry is not evidence of a listed superficial Rockwell component-testing service. [4]
Where the required specimen category, method or scale does not explicitly match, obtain clarification before authorising work. Retain the component-testing entry you are relying on—not simply an accreditation number or machine-calibration capability.
4. Agree on preparation and test locations
“Prepared metallic test specimens” is a scope category used by Perth NDT, Victorian Testing and AMTS. [2][3][4] Ask the laboratory to confirm who performs cutting, grinding, polishing or mounting and agree on a preparation-approval procedure.
NIST’s US Rockwell guide, published more than three years ago and used here as technical background—not an Australian laboratory option or a current Australian requirement—describes testing as relatively non-destructive: it leaves a small indentation. It also addresses surface preparation and measurement locations as factors relevant to measurement variability. [1]
Include these recommended customer instructions:
- What may be tested: the supplied component or an authorised specimen extracted from it.
- Preparation permissions: permitted and prohibited operations. Avoid “prepare as necessary” if material removal needs your approval.
- Condition and protected areas: material, geometry and surface condition, with photographs or an annotated drawing showing proposed test areas and surfaces to leave untouched.
- Locations and readings: reproduce the purchase specification’s requirements. If it does not define them, request a proposed test plan for agreement rather than inventing a sampling rule.
A recommended hold instruction is: “Do not undertake preparation or change test locations beyond the agreed permissions without written authorisation.” Ask the laboratory to assess whether the component’s geometry, finish and permitted locations allow the specified work before agreeing to the plan.
5. Specify direct or correlated Rockwell results
State whether the purchase requirement calls for a direct Rockwell measurement or permits a correlated value. NIST explains that Rockwell measures indentation-depth differences; the result depends on the indenter and applied-force combination, so “Rockwell hardness” alone does not identify the scale. [1]
A correlated Rockwell number comes from another measurement principle. NIST recommends identifying the measurement-device type alongside correlated values so the recipient can understand how they were obtained. [1]
If correlated values are proposed, request the original measurement method, device type and documented correlation basis for assessment against the material and purchase specification. This is a recommended customer control extending NIST’s device-identification recommendation. [1]
LMATS describes Melbourne and Sydney laboratory testing, portable Rockwell/Vickers equipment and on-site hardness services. These are vendor-reported capabilities. [5] LMATS also reports accreditation; ask it to provide the applicable NATA scope entry and confirm the Rockwell scale and measurement principle proposed for each portable result. [5] Ask for the proposed method and applicable scope entry; assess any proposed correlation separately against the purchase requirement.
6. Define report identification and traceability
Agree on report content with the order. Ask Perth NDT, Victorian Testing, AMTS or LMATS to confirm the report fields for the proposed testing. [2][3][4][5] Treat the following as recommended contractual content:
- Component identity: sample identifiers linked to the component, part number and applicable heat or batch identification.
- Requirement references: drawing and revision, purchase specification, and test standard and edition used.
- Work performed: preparation and test locations linked to the marked drawing or location identifiers.
- Results: Rockwell scale, individual readings distinguished from any average or agreed summary, and deviations from the instructions.
- Correlated results: clear identification of their status, measurement-device type and the supporting basis requested in the order.
NIST explains that Rockwell hardness numbers are reported without units; the scale remains necessary to identify the indenter and force combination. For correlated Rockwell values, it recommends reporting the measurement-device type. [1]
If you want a pass/fail statement, agree the acceptance criterion and how the laboratory will reach that decision before testing. Request equipment identification, uncertainty or specific traceability wording explicitly. AMTS’s machine-calibration capability is a separate service, not a promise that calibration details automatically appear on a component-test report. [4]
7. Assemble the order and check the returned report
Use this recommended handover block to bring the instructions together:
- Scope match: record the laboratory and site, component-testing entry, specimen category, method and scale.
- Component IDs: include sample, part, heat/batch and purchase-order references.
- Attached requirements: attach the drawing and revision, purchase specification, method and edition, scale, acceptance limits and applicable clause.
- Preparation: specify allowed work, prohibited alterations and changes requiring written agreement.
- Test plan: identify marked locations, excluded areas and specified readings.
- Result instruction: state whether direct measurement is required or a correlated result is expressly accepted under the specification.
- Report: request identity, requirement references, preparation, locations, results, deviations and any required conformity assessment.
- Exceptions: record any departure, proposed resolution and written agreement.
Before authorising testing, request written confirmation of the method, scale, specimen category and any departure from the order. Resolve an unmatched scope entry, unspecified scale, prohibited preparation or unaccepted correlated result first.
When the report arrives, check component identity, then method, scale, locations, preparation and deviations against the order. For correlated values, look for the device type and supporting basis requested. Compare results with the purchase-specification limits without introducing a scale conversion or tensile-strength inference lacking a documented basis accepted for the material.
If identity is unclear or work differs from the order, obtain clarification rather than assuming equivalence. Retain the scope entry, agreed order and returned report together as the record of coverage, authorisation and results.
References
- NIST recommended practice guide : Rockwell hardness measurement of metallic materials (nist.gov)
- Perth NDT and Mechanical Testing Laboratory – Accredited Organisation (Site No. 12418) – NATA (nata.com.au)
- Victorian Testing and Inspection Services – Melbourne Laboratory – Accredited Organisation (Site No. 18865) – NATA (nata.com.au, 2010)
- Advanced Materials Testing Services Pty Ltd – Accredited Organisation (Site No. 24442) – NATA (nata.com.au, 2018)
- Hardness Test – LMATS (lmats.com.au)