HROUS
How to Choose Heat Exchanger Eddy Current Testing for US Plants
Require a heat-exchanger tube inspection quote to define material suitability, probe access, calibration, coverage, tube-level reporting and responsibilities—not merely a price labeled “eddy current testing.” Use the following as procurement requirements, not as a statement of legal requirements:
- Required in the base quote: method justification, preparation assumptions, examination scope, calibration evidence, reporting outputs, responsibility assignments and commercial terms.
- Separately authorized when needed: supplemental examinations, additional cleaning, reruns and repair work.
Choose the method from the tube alloy and damage concern
Give the contractor the exchanger identity, tube alloy, dimensions, geometry and known condition concerns. Ask it to identify missing information before selecting a method and explain why the proposed technique suits the material and suspected damage.
Applus+’s US service page illustrates why this matters: it limits conventional eddy current testing (ECT) to non-magnetizable tubing, such as brass, titanium and most stainless steels. For magnetizable tubing, including carbon steel and duplex steel, it offers Remote Field Testing (RFT) and magnetic-saturation eddy current methods. It also offers ultrasonic IRIS for either magnetic class.[3]
Require one scope statement connecting three points:
- Method: the proposed inspection technique and probe.
- Material suitability: why it is appropriate for the identified alloy and magnetic behavior.
- Damage objective and limits: which suspected conditions it will assess and which it may not reliably characterize.
Be specific about the damage question. Applus+ describes its bobbin-coil ECT service as detecting and sizing internal and external pits, wall loss and baffle wear—not as a universal solution for every tube condition.[3] Ask whether screening alone answers the question or whether selected findings need confirmation by another technique.
Verify probe suitability and physical access
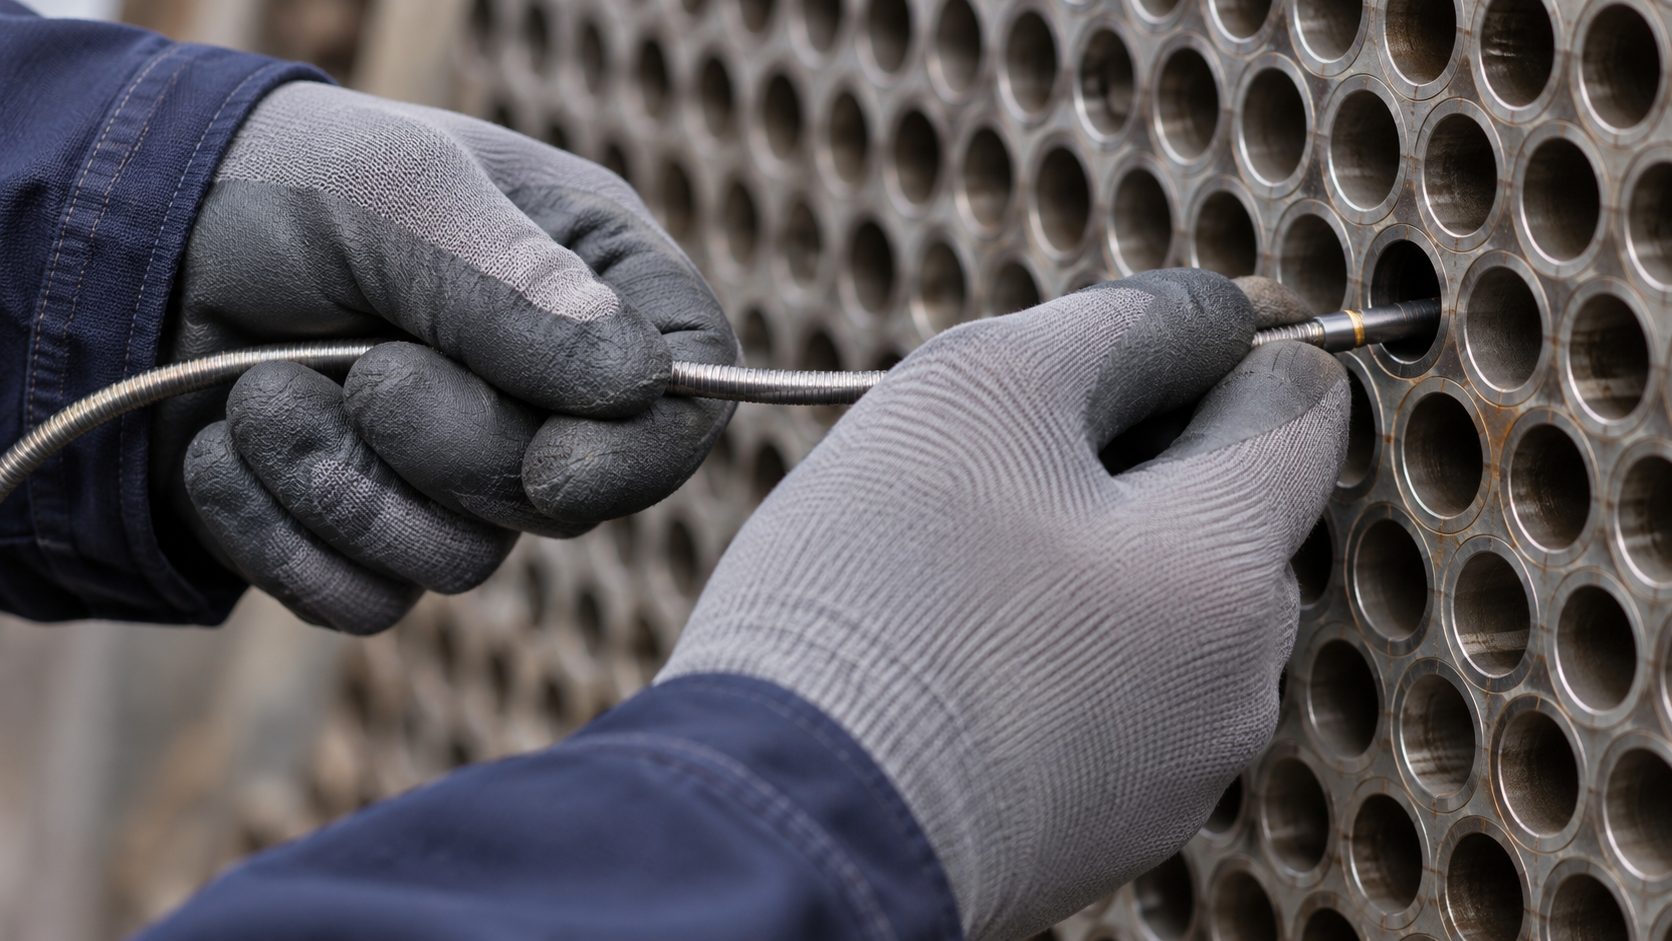
Require the quote to name the probe type and diameter, identify geometry restrictions, and explain how the probe will reach the intended tubes. Applus+ describes internal bobbin-coil examination; ask the contractor to justify its selection against the tube geometry and damage concerns.[3]
Probe access and flaw sensitivity are separate checks. IRISNDT warns that some probe types can miss circumferential cracks, ferromagnetic deposits can distort assessments, and tubes must be obstruction-free.[6] IRISNDT lists an 80% minimum probe fill factor for maximum defect sensitivity and a ±10% variance in call accuracy assessments.[6] Before using either figure to compare bids, require the contractor to define the metric, explain how it is measured, and state whether it applies to the proposed probe, tubing and damage types.
Have the contractor answer these questions in writing:
- What tube dimensions, restrictions and entry clearances does the proposed probe require?
- Which anticipated flaw orientations can it address, and what limitations remain?
- How will blocked or otherwise uninspectable tubes be identified, and is another examination proposed?
Settle these access conditions before accepting the scope. Assign responsibility for opening, cleaning and isolation separately.
Define coverage by tube count, length and circumference
Full-bundle, full-length and full-circumference are different scope descriptions. MISTRAS describes full-length recording for its twisted-tube inspection equipment; EddyTech ECS describes examination of the entire tube circumference. Neither description alone answers all three coverage questions.[1][2]
- Which tubes? State the total bundle tube count and planned examination count. For sampling, require the selection basis and identify the included tubes—not simply “representative coverage.”
- Which portions? Specify the intended examination length and require a record of unexamined segments. Full-length recording does not establish how many tubes will be examined.
- What circumferential scope? Require the probe’s examination scope and detection limitations. IRISNDT’s background-only technical guidance advertises 100% surface examination with 360-degree coverage through the length while warning that some probes can miss circumferential cracks.[6]
Make a coverage exception record a deliverable: identify each inaccessible tube and unexamined segment, the reason, and the proposed disposition. Agree who approves reduced coverage or an alternative examination before the scope changes.
Use this scope-sheet entry:
Record the planned and total tube counts, sampling basis, intended examination length, circumferential scope, exclusions, detection limitations, exception-record requirements and scope-change approval process.
Request calibration evidence and sizing limitations
Pair coverage requirements with documented calibration. MISTRAS says calibration against reference standards made from the same or very similar material is critical and names an “ASME tubing pit standard.”[1] Ask MISTRAS to confirm availability for the plant.
Applus+ describes comparison with reference pieces containing artificial defects of known dimensions, such as notches of known depth or holes of known diameter.[3] Request these details:
- Reference standard: identification, material relationship to the tubes, and artificial-defect types and dimensions.
- Procedure and records: applicable inspection procedure, standard edition, calibration-block drawing, verification arrangements and calibration documentation.
- Sizing limitations: uncertainty for the relevant damage types, distinguishing estimated dimensions from any project-specific sizing guarantee.
Do not treat the vendor’s ASME reference as an acceptance criterion. Ask the contractor to identify the specific provisions supporting its procedure and the agreed basis for evaluating findings.
Specify a tube map and locatable findings
A report is not automatically a usable tube map. Applus+ and EddyTech describe recorded findings and reports but do not expressly promise a map or tube-numbering convention.[2][3] Before data acquisition, agree on exchanger identification, tubesheet viewing orientation, row-and-tube numbering, and the coordinate reference. Ask the contractor to show how an indication will be located on the physical bundle.
Specify a minimum tube-level record:
- Identity: exchanger and tube ID matching the agreed map.
- Examination status: examined, partly examined or unexamined, with unexamined segments identified.
- Location: indication position, reference end and measurement units.
- Finding: indication category and supported dimensions or wall-loss estimate, with limitations.
- Follow-up: review status and supplemental examination results linked to the original record.
Require definitions for indication categories rather than assuming standardized severity colors. Applus+ describes internal and external pits, localized and gradual wall loss, and baffle wear—examples the reporting scheme should distinguish when applicable.[3]
Request a sample report and tube map, then specify PDF and machine-readable outputs. Treat editable exports, underlying inspection data, retention periods and trending formats as requested deliverables, not assumed commitments.
Set a delivery deadline. Applus+ says heat-exchanger tube indications are assessed onsite and entered into reporting software, with reports typically available immediately after inspection.[3] Put the project’s required turnaround in the quote rather than relying on typical availability.
Keep future inspection scheduling separate from report-delivery requirements. EddyTech recommends eddy current testing at least every 3 years in open-loop systems, such as most condenser water loops, and every 6 years in closed-loop systems, such as most chilled water loops.[2] These recommendations concern when to inspect again, not when reports are due or which data the contractor will deliver.
Assign preparation and outage responsibilities
Assign a named party—not simply “by others”—for isolation, draining, opening covers or channel heads, cleaning, access, readiness acceptance and restoration. These are negotiated assignments, not duties automatically included in an inspection price.
- Define the handoff condition. Specify tube cleanliness and access requirements, who checks readiness, and who authorizes inspection to begin.
- Assign additional preparation. Agree who handles further cleaning or blocked-tube work and who accepts the tubes afterward.
- Identify access work. State whether bundle removal or other work is included, excluded or separately authorized.
Admiralty Industries provides tube/material and maintenance guidance rather than a comparable inspection-service offer.[5] Its guidance says cleaning selection should reflect fouling, accessibility and alloy. It also notes that mechanical cleaning of fixed-tubesheet exchangers is generally tube-side only, with shell-side access requiring bundle removal.[5]
Keep preparation and any required post-cleaning testing subject to the equipment’s applicable requirements. OXMAINT, a maintenance-management software vendor based in Sunnyvale, California, says OEM instructions, the water-treatment program and applicable pressure-vessel requirements take precedence over its general maintenance checklist.[4]
Set follow-up rules without delegating repair acceptance
Name the plant contact, notification route, escalation timing and person authorized to approve supplemental examinations. Define these before the outage rather than leaving the inspection crew to resolve approvals.
Choose follow-up according to the indication and engineering review. EddyTech describes borescope inspection or metallurgical analysis for flagged tubes.[2] Admiralty’s maintenance guidance describes full-bundle ECT or RFT screening followed by targeted IRIS wall-thickness confirmation.[5] Ask the contractor to justify any proposed sequence and price the supplemental work separately.
Keep findings separate from repair acceptance. Require the contractor to distinguish observations, interpretations and recommendations. Reserve plugging, replacement, repair acceptance and return-to-service decisions for the responsible engineer, using the project’s agreed acceptance basis. OXMAINT’s general guidance likewise defers to OEM instructions, water-treatment requirements and applicable pressure-vessel codes.[4]
- Identify who authorizes each follow-up examination.
- Assign responsibility for revised records after supplemental analysis.
- Document plugging or replacement against the agreed tube identifiers, with engineering disposition separate from inspection classification.
Request an itemized quote and change terms
Applus+ offers a US quote-request route.[3] Ask Applus+ to confirm job prices, mobilization charges, overtime rates, minimums, lead-time commitments and cancellation terms in writing. Ask for an itemized price tied to the defined scope.
Require bidders to identify the pricing basis: tube count, examination scope, preparation condition, personnel and equipment, travel, standby, reruns and supplemental examinations. Mark each item as included, excluded or separately chargeable.
Request written scheduling, report-delivery, rescheduling, cancellation and quote-validity terms. Define who can authorize changes, how additional charges are approved and whether added work changes delivery dates. Ask for proposed personnel, qualifications and the applicable inspection procedure rather than inferring certification from a general service description.
Attach the scope sheet to the RFQ and request marked exceptions covering:
- Material, method and probe suitability.
- Access, preparation and restoration responsibilities.
- Coverage, exclusions and exception records.
- Calibration evidence and sizing limitations.
- Tube identifiers, defect locations and report outputs.
- Follow-up authorization and engineering disposition.
- Price, deliverables and change terms.
Resolve gaps in material suitability, coverage, finding location and responsibility before treating quotations as equivalent. Compare the defined work—not merely the totals.
References
- Eddy Current Inspection Services | MISTRAS Group | MISTRAS Group (mistrasgroup.com)
- Services (eddytechecs.com)
- Eddy current testing | Eddy current inspection | Applus+ USA (applus.com)
- HVAC Heat Exchanger Maintenance Checklist and Inspection Guide (oxmaint.com)
- Heat Exchanger Maintenance: A Practical Guide for Engineers | Admiralty Industries (admiraltyindustries.com, 2026)
- Eddy Current Testing of Heat Exchanger Tubes (irisndt.com, 2024)